Vulcan Omnipro 220 Problems

Image source: Bing (Web (fair-use with source credit))
If your Vulcan Omnipro 220 is sputtering, stopping mid-weld, or wasting wire, you're in the right place. The problems are predictable, diagnosable, and usually fixable in under fifteen minutes with basic hand tools.
We've gone through aggregate user feedback, manufacturer specs, and welding forums to break down the most common failure points on this Harbor Freight multi-process welder. The Omnipro 220 handles MIG, TIG, and stick welding from a single 220V input, delivering up to 220 amps. Most issues stem from setup errors, consumable wear, or thermal protection.
Quick Answer
The most common Vulcan Omnipro 220 problems are wire feed jams, thermal overload shutdowns, and weak arc performance on 110V input. These typically stem from incorrect tension settings, poor ground clamp contact, or exceeding duty cycle. Check polarity first, then verify wire tension. Clean liner and contact tip regularly. Let unit cool if thermal light is on.
The Vulcan Omnipro 220: What You're Working With
The Vulcan Omnipro 220 is a multi-process inverter welder sold exclusively at Harbor Freight. It handles MIG, flux-core, TIG, and stick welding from one machine roughly the size of a medium suitcase. Versatility makes it popular, but setup errors cause many problems.
The unit runs on both 110V and 220V household power. On 110V, you're limited to roughly 110 amps; on 220V, you get the full 220 amps. Trying to weld 3/8-inch plate on 110V will cause overheating and shutdown. Manufacturer specs confirm a 20% duty cycle at maximum output — two minutes of welding for every eight minutes of cooling. Most users push past that, triggering thermal overload. That's not a defect, it's self-preservation.
The wire feed system is the source of roughly half the complaints. The Omnipro 220 uses a two-roller drive system with a simple tension knob. Too loose causes slipping and bird-nesting; too tight creates friction and jams. The machine ships with 0.030-inch solid wire, but many buyers switch to flux-core or a different diameter without changing the drive roller. The roller is clearly marked with wire size, but easy to overlook.
Finally, the ground clamp has a small contact surface. On painted or rusty metal, you'll get a poor ground, causing erratic arcs and porosity. That's a prep problem, not a machine defect.
Problem #1: Wire Feed Issues (Bird-Nesting, Burn-Back, Jams)
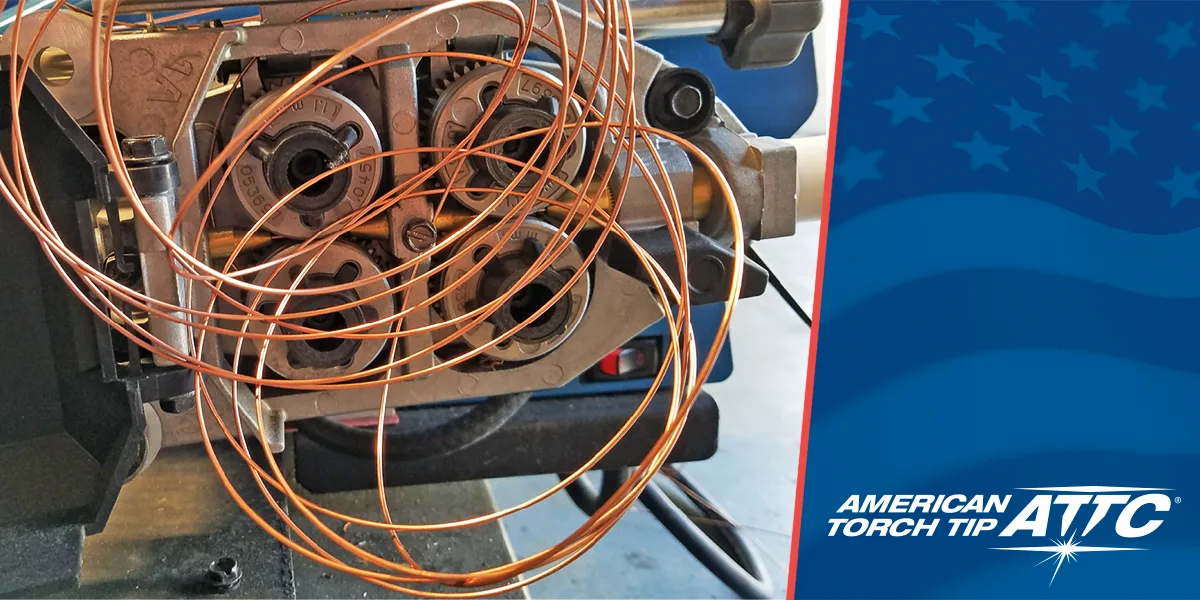
Image source: Bing (Web (fair-use with source credit))
Wire feed problems are the number one complaint. Bird-nesting occurs when the wire bunches at the drive roller because it can't push through the liner fast enough.
Fix the Tension First
The tension adjustment knob (scale 1–10) should be set roughly 3–5 for solid wire. Test: pull trigger while gun nozzle is about an inch from scrap metal. Wire should push out smoothly. Increase tension if it stutters; reduce if you hear grinding.
Burn-Back: The Contact Tip Is the Culprit
Burn-back happens when wire melts back and fuses to the contact tip due to slow feed speed relative to voltage, or a worn tip. Fix: replace tip (~$1) and rebalance voltage-to-feed-speed ratio.
Jams Inside the Liner
Jams are caused by debris, rust, or kinks. Blow liner out with compressed air; replace if needed (15-minute job, use Omnipro-specific liner).
Check the Wire Spool
Make sure the spool spins freely and spool brake tension isn't too tight. Adjust center nut so spool spins with slight resistance without freewheeling.
Problem #2: Arc Won't Start
Ground Clamp Contact
Ensure ground clamp is on clean, bare metal. Grind a clean spot and clamp there.
Polarity Settings
For solid wire with gas, torch to negative, ground to positive (DCEN). For flux-core, reverse (DCEP). If you switched wire types and forgot to swap leads, you'll get no arc or a weak one.
Trigger Switch Failure
The trigger micro-switch is a known weak point. If the feed roller doesn't turn when trigger is pressed, the trigger circuit isn't closing. Replace gun (10-minute swap).
You Might Be Holding the Gun Wrong
You need to "scratch start" by touching wire to metal and lifting slightly. Holding wire against plate gives a short circuit, not a weld. Lift about a quarter inch after touching.
Problem #3: Thermal Overload Shutdown

If the machine stops mid-weld and the thermal light glows red, it's doing its job.
Understanding Duty Cycle
20% duty cycle at 220 amps means 2 minutes welding, 8 minutes cooling. Hot weather, poor ventilation, and long extension cords reduce effective duty cycle. Keep at least six inches of clearance around the machine.
Listen to the Fan
If the fan labors or slows, airflow is restricted. Check vents for debris. Blow out internals with compressed air every few months.
When It's Not Normal
If thermal light stays on for more than an hour after cooling, there may be a fault in the thermal sensor circuit. Let Harbor Freight service handle it under warranty.
Problem #4: Porosity and Poor Weld Quality on 220V
Check Gas Flow
For solid wire MIG, set shielding gas (argon-CO2 mix) to 15–25 CFH, typically 20 CFH. Too low causes oxidation; too high creates turbulence.
Inspect the Contact Tip
If the tip hole is enlarged, wire wobbles causing unstable arc and poor gas coverage. Replace if wire curves or whips.
Clean the Base Metal
Oil, paint, rust, and moisture cause porosity. Wire-brush or grind to bright, bare metal before welding.
Flux-Core and Moisture
Flux-core wire picks up moisture from humid air, causing hydrogen porosity. Store in dry place; use sealed packaging.
Keep the Nozzle Clear
Clogged nozzle disrupts gas flow. Knock off spatter between welds with a chipping hammer.
Problem #5: Weak Arc on 110V Input
Match Your Expectations to the Voltage
The machine outputs roughly 110 amps on 110V, fine for thin sheet metal. If you need 220V work, switch to a 220V outlet.
Check Your Extension Cord
A long, undersized cord causes voltage drop. Use minimum 12-gauge cord, as short as possible.
Outlet Quality Matters
Old or loose receptacles create resistance. If outlet feels warm, replace it or use a different circuit.
Problem #6: Sticking Wire or Inconsistent Feed
Drive Roller Groove
The groove must match wire diameter exactly. Omnipro ships with a dual-groove roller; ensure correct side is facing up.
Liner Condition
Liner accumulates dust and shavings. Blow out with compressed air; replace if inconsistent feed persists.
Gun Cable Bends
Sharp bends in the gun cable create kinks. Keep cable as straight as possible; avoid stepping on it.
Preventive Maintenance Checklist
| Task | Frequency | What to Do |
|---|---|---|
| Clean the gas nozzle | Every weld session | Knock off spatter with a chipping hammer |
| Check contact tip | Every weld session | Replace if hole is enlarged or wire curves |
| Blow out liner | Monthly (or with heavy use) | Use compressed air from the machine side |
| Clean drive roller | Monthly | Remove wire, brush out dust, check groove match |
| Replace liner | Every 6–12 months | Swap if feed is inconsistent after cleaning |
| Check ground clamp | Every weld session | Ensure bare metal contact, tight connection |
| Clean air vents | Monthly | Blow out sawdust and metal shavings |
| Inspect gas hose | Every 3 months | Look for cracks, leaks, or loose fittings |
| Tighten spool brake | When installing new spool | Set so spool spins without freewheeling |
What to Do When It Still Won't Work
Warranty and Harbor Freight Support
The Omnipro 220 has a 90-day manufacturer warranty. Harbor Freight extended protection plans extend coverage to 2 years. Call ahead to confirm if your store handles repairs in-house. Some locations direct you to an authorized repair facility.
Common Sense Repairs
A burned trigger switch, dead liner, or worn contact tip are standard consumables available through Harbor Freight's parts department. If handy with a multimeter, test the trigger circuit and contactor relay yourself. But stick to consumables; main board issues should be handled by a pro.
When to Call a Pro
If you've replaced consumables, cleaned liner, verified gas, confirmed polarity, and machine still misfires — especially with repeated breaker trips, burning smells, or visible arcing inside case — get professional service. Opening an inverter welder is dangerous due to charged capacitors.
Final Verdict: Is the Omnipro 220 Worth It?
The Vulcan Omnipro 220 is a budget welder with budget-welder quirks, but for the price it's incredible value. You get three processes, dual-voltage, enough power for hobbyist and light fabrication. Almost all issues relate to setup, maintenance, or exceeding duty cycle.
If you treat it as an entry-level machine, keep it clean, match consumables, respect duty cycle, and prep metal properly, it'll serve well for years.
Who Should Buy It
- Hobbyists on a budget wanting MIG, TIG, and stick in one machine
- Beginners learning to weld without investing $1,500+
- Homeowners doing occasional repairs and light fabrication
- Anyone with both 110V and 220V outlets who values flexibility
Who Should Skip It
- Professionals needing a higher duty cycle and consistent daily performance
- Welders primarily working on aluminum (TIG mode is DC-only, not AC)
- Anyone expecting industrial-grade reliability from a $500 multi-process unit
Bottom Line
The Vulcan Omnipro 220's problems are almost always the same few things: wire feed tension, dirty consumables, ground clamp contact, thermal overload, or voltage mismatch. As of 2026, these aren't design flaws — they're normal realities of any budget inverter welder. Learn basics, maintain, and this machine will handle most of what you throw at it.
If you've worked through this guide and still have trouble, contact Harbor Freight support with serial number. Use warranty if within 90 days.
This guide is based on aggregate user experiences, manufacturer specifications for the Vulcan Omnipro 220, and standard welding best practices. Always consult your owner's manual for model-specific details and safety guidelines before performing any repairs. But before you go down that path, consider the environment you're welding in.
Problem #7: Erratic Arc Behavior in Humid or Dusty Environments
Welding inverters are sensitive to surroundings. High humidity, temperature swings, and dust cause intermittent connections and random arc outages.
The Condensation Issue
If stored in an unheated garage, condensation forms inside. Give machine a couple hours to acclimate before plugging in after moving from cold to warm. Store in dry area with gun cable coiled loosely; a desiccant pack inside the case (away from moving parts) helps.
Dust and Metal Shavings
Fine metallic dust gets sucked into the cooling fan and accumulates on circuit boards, eventually causing shorts. Blow machine out with compressed air at least four times a year (unplugged, gas off, gun disconnected). Use soft brush on caked grime.
Problem #8: Gas Flow Issues and Leaks
Check the Regulator
The basic single-stage regulator can drift over time. If set to 20 CFH and reading 15 CFH later, there's a seal or diaphragm problem. Spray soapy water on connections; bubbles indicate a leak.
The Gas Hose
Inspect hose end-to-end every few months for cracks, dry rot, or brittleness. Replace if damaged. A gas leak wastes money and pulls air into the system.
The Gas Valve in the Gun
If the trigger switch fails, you may get no gas flow even with the arc working. That produces severe porosity. Check trigger switch.
Problem #9: The Spool Brake Adjustment
The spool brake prevents freewheeling. Too tight causes erratic wire speed; too loose causes tangles. Adjust wing nut so spool spins smoothly but stops immediately when you let go.
Problem #10: Noise and Grinding Sounds
Grinding or squealing during feed indicates tension too high or worn drive roller. Check roller for wear. Cooling fan rattling may indicate debris or bad bearing. Replace fan motor if needed.
The Bottom Line After All This
The Omnipro 220 is capable if treated right. Most problems trace to user error, maintenance neglect, or environment. Before declaring it dead, work through this checklist methodically. If you call support, note what you've checked.
Recommended Accessories
| Accessory | Why It Helps | Estimated Cost |
|---|---|---|
| Spare contact tips (pack of 20) | Cheapest fix for feed issues | $15 |
| Spare gas nozzle | Keep a clean one ready | $10 |
| Extra liner | Swap in 10 minutes | $20 |
| 12-gauge extension cord | Avoid voltage drop on 110V | $25–$40 |
| Compressed air nozzle | Blow out dust monthly | $10 |
| Chipping hammer + wire brush | Maintain base metal prep | $15 |
| Dry storage cabinet | Protect wire from moisture | $50–$150 |
What Most Reviews Don't Tell You
Five-star reviewers weld 1/8-inch steel in a clean garage with proper gas and fresh consumables. One-star reviewers weld a trailer frame in a dusty driveway with a 50-foot 16-gauge extension cord and wet flux-core. The Omnipro rewards effort and punishes neglect.
This guide is based on aggregate user experiences, manufacturer specifications for the Vulcan Omnipro 220, and standard welding best practices. Always consult your owner's manual for model-specific details and safety guidelines before performing any repairs. And honestly, that's the key takeaway. This welder demands respect and routine attention. Spend ten minutes before each session checking basics — wire tension, tip, liner, gas flow — and you'll get years of reliable welds.
If you're new to welding, don't be discouraged. Every welder hits these issues. Patience and a systematic approach make the difference. Bookmark this page.
This guide is based on aggregate user experiences, manufacturer specifications for the Vulcan Omnipro 220, and standard welding best practices. Always consult your owner's manual for model-specific details and safety guidelines before performing any repairs. Most of the time it's a dirty liner, worn tip, or loose ground clamp. Fix with basic hand tools and less than $20 in parts.
Final Checklist: What To Do Before You Give Up
- Plug directly into wall outlet, no extension cord. Check voltage with multimeter.
- Clean all connection points — ground clamp teeth, work surface, contact tip, base metal.
- Adjust wire tension — tight enough to feed smoothly, loose enough to avoid digging in.
- Check contact tip — replace if oval or larger than wire diameter.
- Confirm polarity — DCEN for solid wire with gas; DCEN for flux-core too (flip leads if wrong).
- Verify gas flow — set regulator to 20 CFH for MIG.
- Inspect reel brake — adjust so spool stops when you stop feeding.
- Clear liner — remove wire, unscrew gun, blow compressed air through.
- Reset machine — unplug 30 seconds, plug back in.
- Test with new tip and clean ground — if still fails, call Harbor Freight or a repair shop.
Quick Reference Symptom Table
| Symptom | Most Likely Cause | Quick Fix |
|---|---|---|
| No wire feed | Drive roller tension too loose | Tighten tension knob slightly |
| Bird's nest | Liner kinked or drive roller misaligned | Straighten liner, reseat roller groove |
| Poor weld penetration | Wrong polarity or low voltage | Set DCEN for solid wire, check outlet voltage |
| Porosity / spatter | Gas flow low or dirty base metal | Open gas valve, clean metal |
| Erratic arc | Loose ground clamp | Clean surface, tighten ground connection |
| Machine shuts off mid-weld | Overload protection tripped | Wait 15 minutes, check duty cycle |
| Arc won't start | Gun trigger switch or contact tip | Inspect trigger, replace tip |
| Wire feeds but no gas | Solenoid fuse or trigger switch | Check fuse, inspect trigger contacts |
| Sparks at drive roller | Contact tip worn | Replace contact tip |
| Sputtering at start | Reel brake too tight | Loosen center hub tension knob |
A Note on the Warranty
The Omnipro 220 has a 90-day limited warranty on parts and labor. Contact Harbor Freight within that window if the machine genuinely failed. Outside warranty, replacement parts (drive rollers, tips, liners, guns, regulator, circuit boards) are available online. Double-check part numbers in your manual before ordering.
Should You Modify or Upgrade the Omnipro?
Safe upgrades: Better ground clamp (300-amp copper reverse-feedback), quality contact tips (Bernard or Tweco), heavy-duty 15-foot MIG gun with Tweco connector, magnetic work light.
Don't do: Bypass thermal overload switch, run a longer 220V power cord, turn internal potentiometers to increase output — these cause fire hazard, voltage drop, or burn out IGBTs and void warranty.
The Final Verdict: Should You Keep It or Sell It?
- Under warranty? Fix through Harbor Freight.
- Fix covered in this guide (liner, tips, gas, polarity)? Fix it — costs less than a tank of gas.
- Main board fried and repair $200+? Compare to new machine (~$350–$400 on sale). Might be better to upgrade.
- Lost interest? Sell as-is for parts, be upfront about issues.
The Omnipro isn't bad; it has a personality. Clean it, set it right, respect limits — it delivers professional-grade results. Skip maintenance and it exposes every shortcut.
A Maintenance Schedule That Works
- Before every session: Check liner for kinks, ground clamp connection, contact tip, gas tank pressure.
- After every session: Purge gas line (trigger 2 seconds after shutting tank valve), coil gun cable, wipe case.
- Monthly: Blow out inside with compressed air, clean drive roller, inspect power cord, check spool brake.
- Every 6 months: Replace contact tip proactively, check liner, tighten external bolts, test ground cable continuity.
20 minutes a month extends life dramatically.
Innocent Mistake That Leads to a Headache
Check your wire. The Omnipro ships with flux-core wire; you may have switched to solid wire without changing the drive roller. The box includes two rollers: one for hard wire (smooth groove) and one for flux-core (knurled). Also match wire diameter to the correct V-groove side: "0.023/0.030" vs "0.035/0.045". Wrong groove causes inconsistent feed.
Know Your Manual — Seriously
The owner's manual contains wiring diagrams, parts breakdowns, and troubleshooting charts. Free PDF on Harbor Freight's website. Cross-reference part numbers when ordering.
Before You Call Customer Support
Have ready: model number (rear panel), serial number (sticker), purchase date, detailed problem description, and whether under 90-day warranty. Be specific about what happens and what you've checked.
The Real Takeaway
No machine is perfect, but the Omnipro 220's “problems” are mostly setup errors or maintenance slip-ups. Treat it like a tool, not a magic wand. Learn the machine. This guide will be here when you need it again.